-
About us
 Tianjin lefin Industrial
TIANJIN LEFIN STEEL GROUP containing Tianjin lefin Industrial Co.,Ltd. 、Tianjin lefin steel import & export Co.,Ltd and Tianjin Shengqifeng International Trading Co., Ltd. -
Products
Steel Pipe Processing
Our main products include 1/2inch to 16 inch ERW PIPE/GI PIPE which has been produced according to BS1387/ASTM A53/EN10219/EN10255/EN10217 Standard -
-
Service Capability
Guarantee Quality
Our steel pipes are suitable for oil, natural gas, shipbuilding, chemical industry, water conservancy, electrical, steel structure, construction and other related fields.
- Details
-
Products Description
EN 10217 STEEL PIPE
Standard:EN 10217
Grade: P195GH, P235GH, P265GH
Outside Diameter: 20-660mm
Wall Thickness:1.3-16mm
Length: 5.8,m, 6m, 12m or as your requirement
The Wall Thickness Tolerance: ±5%
Surface Treatment: Bare Finish, Painting, Oiling, Galvanzation, 3PE, FBE coated......
Chemical Composition
Chemical composition(cast analysis)%
Steel Grade
C
Si
max.Mn
P
max.S
max.P195GH
≤0.13
0.35
≤0.70
0.025
0.020
P235GH
≤0.16
0.35
≤1.20
0.025
0.020
P265GH
≤0.20
0.40
≤1.40
0.025
0.020
Physical Requirements
Mechanical properties for wall thickness T≤16
Steel Grade
Tensile properties at room temperature
Upper yield strength MPa
Tensile strength Mpa
Elongation %
longitudinal
transverse
P195GH
195
320-440
27
25
P235GH
235
360-500
25
23
P265GH
265
410-570
23
21
Characteristics
The main characteristics of EN10217 steel pipe
1. Material and performance
• Made of non-alloy steel with high strength and corrosion resistance.
• Excellent compression performance, due to strict welding process control, can meet the needs of high-pressure fluid transportation.
• Smooth surface and precise dimensions, suitable for precision machining (e.g. cutting, welding, etc.).
2. Inspection and reliability
• Ensure product safety and reliability through rigorous quality inspection (e.g. impact testing, chemical composition analysis).
3. Application scenery
• Widely used in oil, gas, chemical and other industries of fluid transport, as well as building structural support.Production And Processing
EN 10217 Steel pipe production and processing
Production process
1. Prepare raw materials
EN 10217 steel tubes are made of unalloyed steel as a base material, usually steel plates or strips, and are subject to chemical composition analysis and surface quality inspection to ensure compliance with standard requirements.2. Molding process
• Straight seam welded pipe (LSAW) : The steel plate is bent into a tube by forming process such as UOE, JCOE or RBE, and then welded by double-sided submerged arc welding (SAW). The UOE process is suitable for high volume production, and the JCOE process is more flexible, especially for high steel grade thick wall pipes.
• Spiral welded pipe (SSAW) : The strip steel coil is helically formed after leveling and pre-bending treatment, and welded by submerged arc welding process, which is suitable for large diameter pipe.
• Resistance welded pipe (ERW) : The use of high frequency current to heat the edge of the tube billet and squeeze welding, suitable for small and medium-sized diameter pipe, high production efficiency.3. Welding and post-processing
• Weld quality inspection (such as ultrasonic flaw detection and X-ray detection) is required after welding.
• Some steel pipes need to be expanded to eliminate residual stress, or to improve mechanical properties through heat treatment such as normalizing (N) and tempering (T).4. Surface treatment and inspection
• Surface polishing, sandblasting or anti-rust treatment to improve corrosion resistance.
• Strict chemical composition analysis, mechanical property testing and non-destructive testing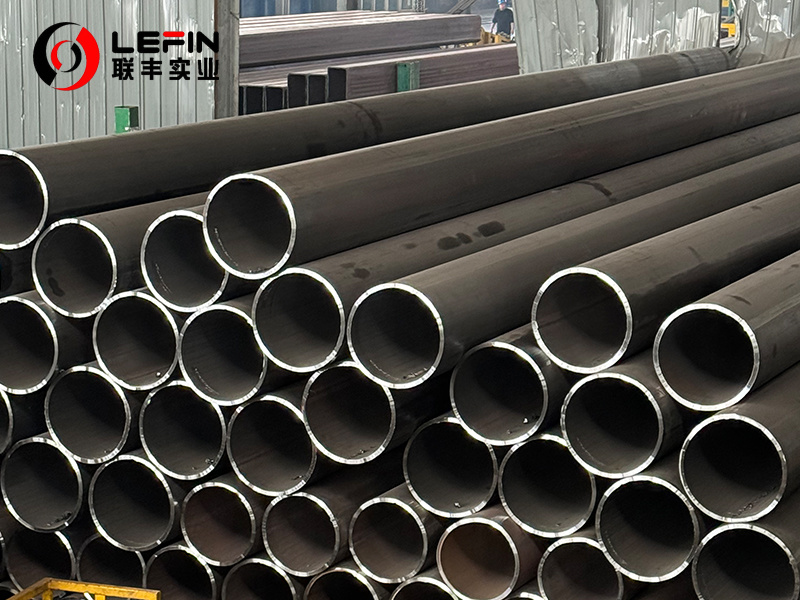
Processing Points
1. Cutting and forming
Plasma cutting, laser cutting or mechanical cutting can be used to ensure smooth incision. Shaped tubes such as square tubes need to be shaped by the mold, such as round tubes and square tubes need to be formed several times under pressure.2. Welding and connection
• Argon arc welding or submerged arc welding is recommended to avoid the risk of intergranular corrosion that may result from high-frequency welding.
• Clean the surface of the oil before welding, and polish the weld bead and anti-corrosion treatment after welding.3. Cold drawing and straightening
The cold drawing process is used to adjust the wall thickness and diameter, which needs to be combined with lubricants to reduce friction; The straightener is used to correct the straightness of the pipe and ensure the installation accuracy.Storage and Use
Storage requirements
1. Environmental control
• Store in a dry, ventilated, rainproof and sunproof warehouse, away from fire sources and corrosive media.
• The pipe must be isolated from the ground with a support (recommended height ≥20cm) to avoid moisture.2. Code arrangement
• Upright: suitable for short pipe, need to use a fixed frame to prevent toppling.
• Lying flat: The long pipe should be placed in layers, and the layers should be padded with non-slip materials (such as rubber pads) to avoid extrusion deformation.3. Perform regular maintenance
• Check whether the anti-rust coating on the surface is intact. If necessary, apply anti-rust oil or place moisture-proof agent.
• Clean surface dust every quarter to avoid oxidative rust.

EN10217 STEEL PIPES
Subcategory
Keyword
- Details
-
Products Description
EN 10217 STEEL PIPE
Standard:EN 10217
Grade: P195GH, P235GH, P265GH
Outside Diameter: 20-660mm
Wall Thickness:1.3-16mm
Length: 5.8,m, 6m, 12m or as your requirement
The Wall Thickness Tolerance: ±5%
Surface Treatment: Bare Finish, Painting, Oiling, Galvanzation, 3PE, FBE coated......
Chemical Composition
Chemical composition(cast analysis)%
Steel Grade
C
Si
max.Mn
P
max.S
max.P195GH
≤0.13
0.35
≤0.70
0.025
0.020
P235GH
≤0.16
0.35
≤1.20
0.025
0.020
P265GH
≤0.20
0.40
≤1.40
0.025
0.020
Physical Requirements
Mechanical properties for wall thickness T≤16
Steel Grade
Tensile properties at room temperature
Upper yield strength MPa
Tensile strength Mpa
Elongation %
longitudinal
transverse
P195GH
195
320-440
27
25
P235GH
235
360-500
25
23
P265GH
265
410-570
23
21
Characteristics
The main characteristics of EN10217 steel pipe
1. Material and performance
• Made of non-alloy steel with high strength and corrosion resistance.
• Excellent compression performance, due to strict welding process control, can meet the needs of high-pressure fluid transportation.
• Smooth surface and precise dimensions, suitable for precision machining (e.g. cutting, welding, etc.).
2. Inspection and reliability
• Ensure product safety and reliability through rigorous quality inspection (e.g. impact testing, chemical composition analysis).
3. Application scenery
• Widely used in oil, gas, chemical and other industries of fluid transport, as well as building structural support.Production And Processing
EN 10217 Steel pipe production and processing
Production process
1. Prepare raw materials
EN 10217 steel tubes are made of unalloyed steel as a base material, usually steel plates or strips, and are subject to chemical composition analysis and surface quality inspection to ensure compliance with standard requirements.2. Molding process
• Straight seam welded pipe (LSAW) : The steel plate is bent into a tube by forming process such as UOE, JCOE or RBE, and then welded by double-sided submerged arc welding (SAW). The UOE process is suitable for high volume production, and the JCOE process is more flexible, especially for high steel grade thick wall pipes.
• Spiral welded pipe (SSAW) : The strip steel coil is helically formed after leveling and pre-bending treatment, and welded by submerged arc welding process, which is suitable for large diameter pipe.
• Resistance welded pipe (ERW) : The use of high frequency current to heat the edge of the tube billet and squeeze welding, suitable for small and medium-sized diameter pipe, high production efficiency.3. Welding and post-processing
• Weld quality inspection (such as ultrasonic flaw detection and X-ray detection) is required after welding.
• Some steel pipes need to be expanded to eliminate residual stress, or to improve mechanical properties through heat treatment such as normalizing (N) and tempering (T).4. Surface treatment and inspection
• Surface polishing, sandblasting or anti-rust treatment to improve corrosion resistance.
• Strict chemical composition analysis, mechanical property testing and non-destructive testingProcessing Points
1. Cutting and forming
Plasma cutting, laser cutting or mechanical cutting can be used to ensure smooth incision. Shaped tubes such as square tubes need to be shaped by the mold, such as round tubes and square tubes need to be formed several times under pressure.2. Welding and connection
• Argon arc welding or submerged arc welding is recommended to avoid the risk of intergranular corrosion that may result from high-frequency welding.
• Clean the surface of the oil before welding, and polish the weld bead and anti-corrosion treatment after welding.3. Cold drawing and straightening
The cold drawing process is used to adjust the wall thickness and diameter, which needs to be combined with lubricants to reduce friction; The straightener is used to correct the straightness of the pipe and ensure the installation accuracy.Storage and Use
Storage requirements
1. Environmental control
• Store in a dry, ventilated, rainproof and sunproof warehouse, away from fire sources and corrosive media.
• The pipe must be isolated from the ground with a support (recommended height ≥20cm) to avoid moisture.2. Code arrangement
• Upright: suitable for short pipe, need to use a fixed frame to prevent toppling.
• Lying flat: The long pipe should be placed in layers, and the layers should be padded with non-slip materials (such as rubber pads) to avoid extrusion deformation.3. Perform regular maintenance
• Check whether the anti-rust coating on the surface is intact. If necessary, apply anti-rust oil or place moisture-proof agent.
• Clean surface dust every quarter to avoid oxidative rust.
Related products
Product Consulting
Address: Hengtai Road,Daqiuzhuang Town,Jinghai County,Tianjin,China
Mob: +8615122229899(whatspp)
Phone: +86 22 58171905
Fax: +86 22 58171902
E-mail:info@lefinsteel.com
Get company updates
Tianjin Lefin Industrial Co.,Ltd. All rights reserved City sub-station SEO www.300.cn