-
About us
 Tianjin lefin Industrial
TIANJIN LEFIN STEEL GROUP containing Tianjin lefin Industrial Co.,Ltd. 、Tianjin lefin steel import & export Co.,Ltd and Tianjin Shengqifeng International Trading Co., Ltd. -
Products
Steel Pipe Processing
Our main products include 1/2inch to 16 inch ERW PIPE/GI PIPE which has been produced according to BS1387/ASTM A53/EN10219/EN10255/EN10217 Standard -
-
Service Capability
Guarantee Quality
Our steel pipes are suitable for oil, natural gas, shipbuilding, chemical industry, water conservancy, electrical, steel structure, construction and other related fields.
- Details
-
Products Description
Standard: EN39
Grade: S235GT
Procedure: SMLS/ ERW
Size: 1 1/2 INCH (48.3MM)
Wall thickness: 3.2/4MM
Length: 6M, 6.4M or customized from 4-12M
Thickness tolerance: ±10%
Surface: Hot dipped galvanised, Pre-galvanized, Black, Painted
Ends: Plan ends, bevel ends, both ends threadings, one with caps, another with couplings, rolled grooved, spigot joint
Shipment ways: Container or bulk vessel
Chemical composition & Physical requirements
Chemical composition and Mechanical Properties
Steel Grade
Chemical composition
Mechanical Properties
C
max.Si
Mn
max.P
max.S
max.Ai
min.Yield strength MPa
Tensile strength MPa
Elongation
%
minS235GT
0.20
a,b
1.40
0.040
0.045
0.020
235
340/520
24
a ≤ 0,05% (range 1) (≤ 0,04% if option 2 is specified) or ≥ 0,15% ≤ 0,25% (range 2). b When bare tubes are specified (see option 8) the range shall be reported at the time of enquiry and order. Processing technology
The processing technology of EN39 steel pipe
1. Surface treatment process
• EP (electrolytic polishing) : The surface of the steel pipe is polished by adjusting the voltage, current and acid composition through the electrochemical principle, improving the finish and removing the oxide layer and impurities.
• BA (bright annealing) : Annealed in a high-temperature argon environment, burning carbon and oxygen impurities on the surface of the steel pipe, forming a bright surface effect, but may present a fog surface texture.
• AP (Pickling treatment) : Acid solutions such as nitric acid and fluorous acid are used to remove oxidation layers and rust, improving surface cleanliness and corrosion resistance.
• MP (Mechanical polishing) : The surface of the steel pipe is polished by polishing wheels and abrasives to achieve a smooth effect, but it may reduce corrosion resistance and require subsequent passivation treatment.2. Hot rolling production process
• Perforation: The Discher perforator is used to improve the metal penetration through a large feed Angle (8~13°), but there is a problem of high energy consumption caused by the rotary cross forging effect.
• Molding and welding: through continuous rolling molding after perforation, using resistance welding, arc welding and other methods to weld into pipes.
• Scaling and straightening: Remove oxide and welding slag, and straighten to ensure dimensional accuracy.
• Cutting and rust removal: After cutting as required, the surface rust is removed by pickling or mechanical scrubbing.3. Other processing technologies
• Straightening: cold straightening and hot straightening, using a press or manual beating (suitable for small pipe diameter below DN50).
• Sleeve wire and bending: thread connection needs sleeve wire (manual and electric), bending process requires bending radius 1.5~4D, and control weld position.Detection
The detection method of EN39 steel pipe
1. Intelligent detection system
• 3D structured light detection: Through high-precision 3D imaging technology to capture the point cloud data of the outer wall of the steel pipe, identify cracks, pores and other defects, the accuracy is up to ±0.03mm, the detection rate is over 95%.
Deep learning models: Automatically classify defects and generate inspection reports to support data traceability and process optimization.
• Real-time processing: The system can count the location, type and size of defects in real time, reducing manual intervention and improving efficiency.2. Traditional test items
Chemical composition analysis: verification of the content of carbon, silicon, manganese and other elements in accordance with the standard (e.g. EN 10219).
• Mechanical performance test: including yield strength (≥235 MPa), tensile strength (340~520 MPa) and elongation (≥24%).
• Size and surface inspection: Ensure that the diameter, wall thickness and surface treatment (e.g., galvanized layer density of 200 to 600 g/m²) are up to standard.
• Non-destructive testing (NDT) : such as ultrasonic or magnetic particle testing to detect internal defects.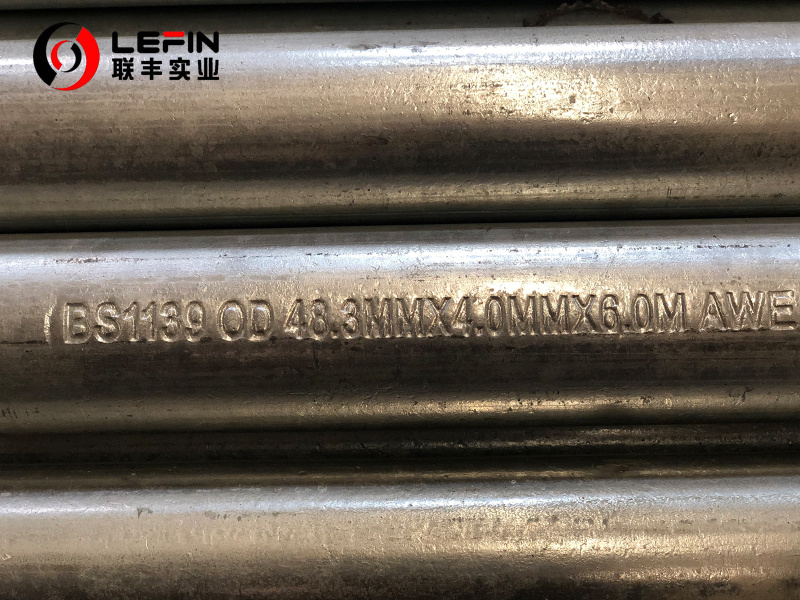

EN39 STEEL PIPES
Subcategory
Keyword
- Details
-
Products Description
Standard: EN39
Grade: S235GT
Procedure: SMLS/ ERW
Size: 1 1/2 INCH (48.3MM)
Wall thickness: 3.2/4MM
Length: 6M, 6.4M or customized from 4-12M
Thickness tolerance: ±10%
Surface: Hot dipped galvanised, Pre-galvanized, Black, Painted
Ends: Plan ends, bevel ends, both ends threadings, one with caps, another with couplings, rolled grooved, spigot joint
Shipment ways: Container or bulk vessel
Chemical composition & Physical requirements
Chemical composition and Mechanical Properties
Steel Grade
Chemical composition
Mechanical Properties
C
max.Si
Mn
max.P
max.S
max.Ai
min.Yield strength MPa
Tensile strength MPa
Elongation
%
minS235GT
0.20
a,b
1.40
0.040
0.045
0.020
235
340/520
24
a ≤ 0,05% (range 1) (≤ 0,04% if option 2 is specified) or ≥ 0,15% ≤ 0,25% (range 2). b When bare tubes are specified (see option 8) the range shall be reported at the time of enquiry and order. Processing technology
The processing technology of EN39 steel pipe
1. Surface treatment process
• EP (electrolytic polishing) : The surface of the steel pipe is polished by adjusting the voltage, current and acid composition through the electrochemical principle, improving the finish and removing the oxide layer and impurities.
• BA (bright annealing) : Annealed in a high-temperature argon environment, burning carbon and oxygen impurities on the surface of the steel pipe, forming a bright surface effect, but may present a fog surface texture.
• AP (Pickling treatment) : Acid solutions such as nitric acid and fluorous acid are used to remove oxidation layers and rust, improving surface cleanliness and corrosion resistance.
• MP (Mechanical polishing) : The surface of the steel pipe is polished by polishing wheels and abrasives to achieve a smooth effect, but it may reduce corrosion resistance and require subsequent passivation treatment.2. Hot rolling production process
• Perforation: The Discher perforator is used to improve the metal penetration through a large feed Angle (8~13°), but there is a problem of high energy consumption caused by the rotary cross forging effect.
• Molding and welding: through continuous rolling molding after perforation, using resistance welding, arc welding and other methods to weld into pipes.
• Scaling and straightening: Remove oxide and welding slag, and straighten to ensure dimensional accuracy.
• Cutting and rust removal: After cutting as required, the surface rust is removed by pickling or mechanical scrubbing.3. Other processing technologies
• Straightening: cold straightening and hot straightening, using a press or manual beating (suitable for small pipe diameter below DN50).
• Sleeve wire and bending: thread connection needs sleeve wire (manual and electric), bending process requires bending radius 1.5~4D, and control weld position.Detection
The detection method of EN39 steel pipe
1. Intelligent detection system
• 3D structured light detection: Through high-precision 3D imaging technology to capture the point cloud data of the outer wall of the steel pipe, identify cracks, pores and other defects, the accuracy is up to ±0.03mm, the detection rate is over 95%.
Deep learning models: Automatically classify defects and generate inspection reports to support data traceability and process optimization.
• Real-time processing: The system can count the location, type and size of defects in real time, reducing manual intervention and improving efficiency.2. Traditional test items
Chemical composition analysis: verification of the content of carbon, silicon, manganese and other elements in accordance with the standard (e.g. EN 10219).
• Mechanical performance test: including yield strength (≥235 MPa), tensile strength (340~520 MPa) and elongation (≥24%).
• Size and surface inspection: Ensure that the diameter, wall thickness and surface treatment (e.g., galvanized layer density of 200 to 600 g/m²) are up to standard.
• Non-destructive testing (NDT) : such as ultrasonic or magnetic particle testing to detect internal defects.
Related products
Product Consulting
Address: Hengtai Road,Daqiuzhuang Town,Jinghai County,Tianjin,China
Mob: +8615122229899(whatspp)
Phone: +86 22 58171905
Fax: +86 22 58171902
E-mail:info@lefinsteel.com
Get company updates
Tianjin Lefin Industrial Co.,Ltd. All rights reserved City sub-station SEO www.300.cn