-
About us
 Tianjin lefin Industrial
TIANJIN LEFIN STEEL GROUP containing Tianjin lefin Industrial Co.,Ltd. 、Tianjin lefin steel import & export Co.,Ltd and Tianjin Shengqifeng International Trading Co., Ltd. -
Products
Steel Pipe Processing
Our main products include 1/2inch to 16 inch ERW PIPE/GI PIPE which has been produced according to BS1387/ASTM A53/EN10219/EN10255/EN10217 Standard -
-
Service Capability
Guarantee Quality
Our steel pipes are suitable for oil, natural gas, shipbuilding, chemical industry, water conservancy, electrical, steel structure, construction and other related fields.
- Details
-
Products Description
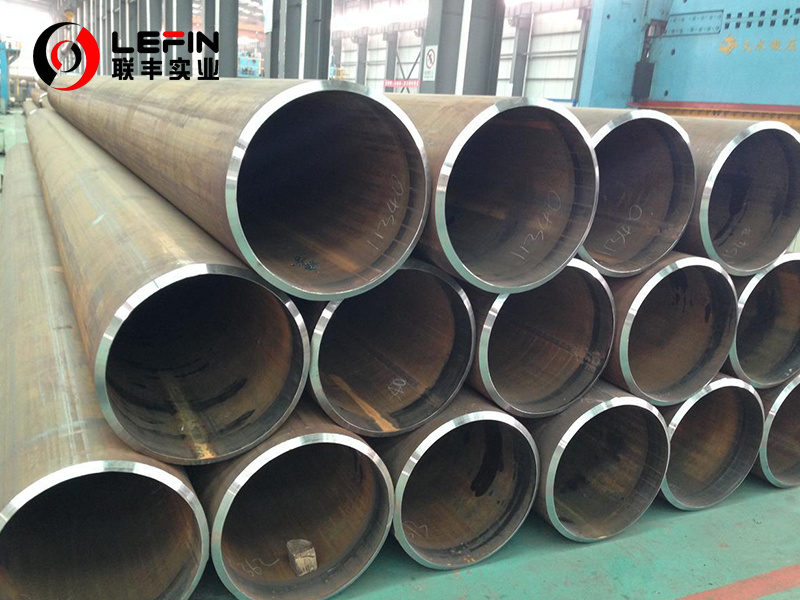
ASTM A53 WELDED PIPE
Standard: ASTM A53
Grade: GR.A, GR.B
Outside Diameter: 20 - 660mm Wall Thickness:1.3 -16 mm
Length: 5.8m, 6m, 12m or as your requirement
Surface Treatment: Painting, Oiling, Galvanized, 3LPE,3PE

Chemical Composition
Chemical Composition,% Electric Resistance Welding Grade C Mn P S Cu Ni Cr Mo V GR.A 0.25 0.95 0.05 0.045 0.4 0.4 0.4 0.15 0.08 GR.B 0.30 1.20 0.05 0.045 0.4 0.4 0.4 0.15 0.08 Carbon (C):
Grade A has a maximum carbon content of 0.25%, while Grade B can have up to 0.30%.
Manganese (Mn):
Grade A has a minimum manganese content of 0.95%, whereas Grade B has a minimum of 1.20%.
Phosphorus (P) and Sulfur (S):
Both grades have a maximum content of 0.05% and 0.045%, respectively.
Physical Requirements
Electric Resistance Welding Grade Tensile strength
MpaYield strength
MpaGR.A 330 415 GR.B 205 240 Detailed Information
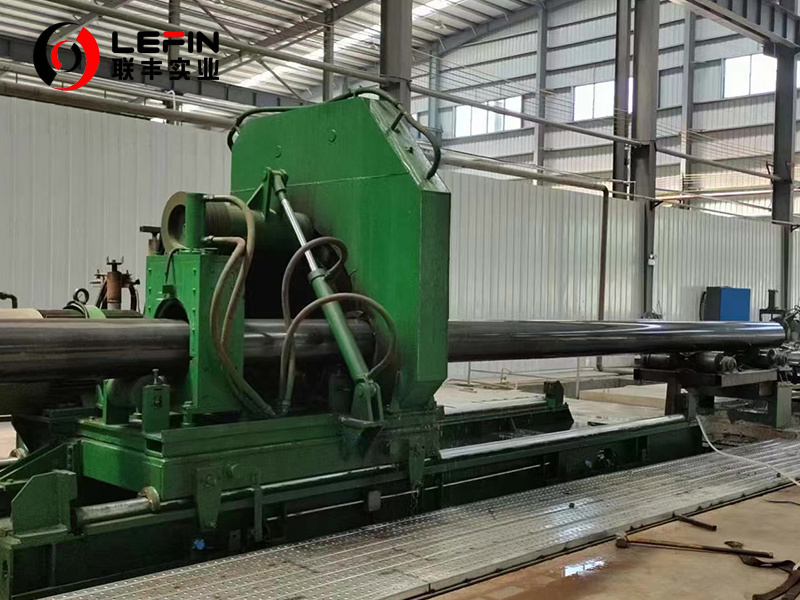
ASTM A53 Welded Pipe is a steel pipe widely used in low pressure fluid transportation and mechanical structures. The specification requirements and key information are as follows:
1. Standard range and type division
Coverage: ASTM A53/A53M-24 standard applies to welded and seamless steel pipes NPS 1/8 to NPS 26 (DN 6 to DN 650), including black (ungalvanized) and hot-dip galvanized types.
Welding type:
Type F (furnace butt welding) : Produced by continuous furnace butt welding process, suitable for ordinary pressure scenarios, but not recommended for flange machining.
Type E (Resistance welding) : The resistance welding process is suitable for mechanical and pressure applications such as steam, water, gas and other piping systems.
2. Material and manufacturing requirements
Chemical composition: Steel must be smelted by open hearth, oxygen converter or electric furnace process, must meet the content limits of carbon, manganese, phosphorus, sulfur and other elements, and may contain copper, nickel, chromium and other alloying elements.
Process control: The welded steel pipe needs to be tested by hydraulic pressure to test the tightness of the weld, and the overall quality needs to be ensured by non-destructive electrical testing. In addition, galvanized steel pipes need to ensure that the zinc layer is uniform to avoid exposure to acid, alkali and salt environments.
3. Mechanical properties and testing
Mechanical properties: Tensile test (verification of tensile strength, yield strength), bending test and flattening test are required to ensure compliance with the mechanical properties specified in the standard.
Quality control: The welded joint needs to be checked for defects such as slag inclusion and sand holes. The galvanized layer needs to be avoided during processing (such as rolling groove and welding), otherwise it needs to be treated with rust prevention.
4. Application Scenarios
Fluid transport: widely used in water, sewage, gas, fire, air and other low-pressure fluid transport systems, as well as mechanical structure support.
Association with other standards: ASTM A53 is often used with GB/T 3091 (Chinese national standard) and BS 1387 (British standard), especially in the field of galvanized welded steel pipes.
5. Processing and installation precautions
Connection mode: Support rolling groove, welding, wire, flange and other connection modes. For example:
Rolling groove connection: Make sure that the groove depth and width meet the standard, and the galvanized layer is not damaged during processing.
Welding connection: Avoid direct spot welding on the surface of galvanized steel pipe. After welding, clean the welding slag on the inner wall and do anti-rust treatment.
Common problems: If the pipe port is not jointed properly or there is sand hole, it is recommended to cut off the problem section and reprocess it. Thread connection should be checked to avoid air leakage and water leakage.
ASTM A53 WELDED PIPE
Subcategory
Keyword
- Details
-
Products Description
ASTM A53 WELDED PIPE
Standard: ASTM A53
Grade: GR.A, GR.B
Outside Diameter: 20 - 660mm Wall Thickness:1.3 -16 mm
Length: 5.8m, 6m, 12m or as your requirement
Surface Treatment: Painting, Oiling, Galvanized, 3LPE,3PE
Chemical Composition
Chemical Composition,% Electric Resistance Welding Grade C Mn P S Cu Ni Cr Mo V GR.A 0.25 0.95 0.05 0.045 0.4 0.4 0.4 0.15 0.08 GR.B 0.30 1.20 0.05 0.045 0.4 0.4 0.4 0.15 0.08 Carbon (C):
Grade A has a maximum carbon content of 0.25%, while Grade B can have up to 0.30%.
Manganese (Mn):
Grade A has a minimum manganese content of 0.95%, whereas Grade B has a minimum of 1.20%.
Phosphorus (P) and Sulfur (S):
Both grades have a maximum content of 0.05% and 0.045%, respectively.
Physical Requirements
Electric Resistance Welding Grade Tensile strength
MpaYield strength
MpaGR.A 330 415 GR.B 205 240 Detailed Information
ASTM A53 Welded Pipe is a steel pipe widely used in low pressure fluid transportation and mechanical structures. The specification requirements and key information are as follows:
1. Standard range and type division
Coverage: ASTM A53/A53M-24 standard applies to welded and seamless steel pipes NPS 1/8 to NPS 26 (DN 6 to DN 650), including black (ungalvanized) and hot-dip galvanized types.
Welding type:
Type F (furnace butt welding) : Produced by continuous furnace butt welding process, suitable for ordinary pressure scenarios, but not recommended for flange machining.
Type E (Resistance welding) : The resistance welding process is suitable for mechanical and pressure applications such as steam, water, gas and other piping systems.
2. Material and manufacturing requirements
Chemical composition: Steel must be smelted by open hearth, oxygen converter or electric furnace process, must meet the content limits of carbon, manganese, phosphorus, sulfur and other elements, and may contain copper, nickel, chromium and other alloying elements.
Process control: The welded steel pipe needs to be tested by hydraulic pressure to test the tightness of the weld, and the overall quality needs to be ensured by non-destructive electrical testing. In addition, galvanized steel pipes need to ensure that the zinc layer is uniform to avoid exposure to acid, alkali and salt environments.
3. Mechanical properties and testing
Mechanical properties: Tensile test (verification of tensile strength, yield strength), bending test and flattening test are required to ensure compliance with the mechanical properties specified in the standard.
Quality control: The welded joint needs to be checked for defects such as slag inclusion and sand holes. The galvanized layer needs to be avoided during processing (such as rolling groove and welding), otherwise it needs to be treated with rust prevention.
4. Application Scenarios
Fluid transport: widely used in water, sewage, gas, fire, air and other low-pressure fluid transport systems, as well as mechanical structure support.
Association with other standards: ASTM A53 is often used with GB/T 3091 (Chinese national standard) and BS 1387 (British standard), especially in the field of galvanized welded steel pipes.
5. Processing and installation precautions
Connection mode: Support rolling groove, welding, wire, flange and other connection modes. For example:
Rolling groove connection: Make sure that the groove depth and width meet the standard, and the galvanized layer is not damaged during processing.
Welding connection: Avoid direct spot welding on the surface of galvanized steel pipe. After welding, clean the welding slag on the inner wall and do anti-rust treatment.
Common problems: If the pipe port is not jointed properly or there is sand hole, it is recommended to cut off the problem section and reprocess it. Thread connection should be checked to avoid air leakage and water leakage.
Related products
Product Consulting
Address: Hengtai Road,Daqiuzhuang Town,Jinghai County,Tianjin,China
Mob: +8615122229899(whatspp)
Phone: +86 22 58171905
Fax: +86 22 58171902
E-mail:info@lefinsteel.com
Get company updates
Tianjin Lefin Industrial Co.,Ltd. All rights reserved City sub-station SEO www.300.cn