-
About us
 Tianjin lefin Industrial
TIANJIN LEFIN STEEL GROUP containing Tianjin lefin Industrial Co.,Ltd. 、Tianjin lefin steel import & export Co.,Ltd and Tianjin Shengqifeng International Trading Co., Ltd. -
Products
Steel Pipe Processing
Our main products include 1/2inch to 16 inch ERW PIPE/GI PIPE which has been produced according to BS1387/ASTM A53/EN10219/EN10255/EN10217 Standard -
-
Service Capability
Guarantee Quality
Our steel pipes are suitable for oil, natural gas, shipbuilding, chemical industry, water conservancy, electrical, steel structure, construction and other related fields.
- Details
-
Brief Introduction
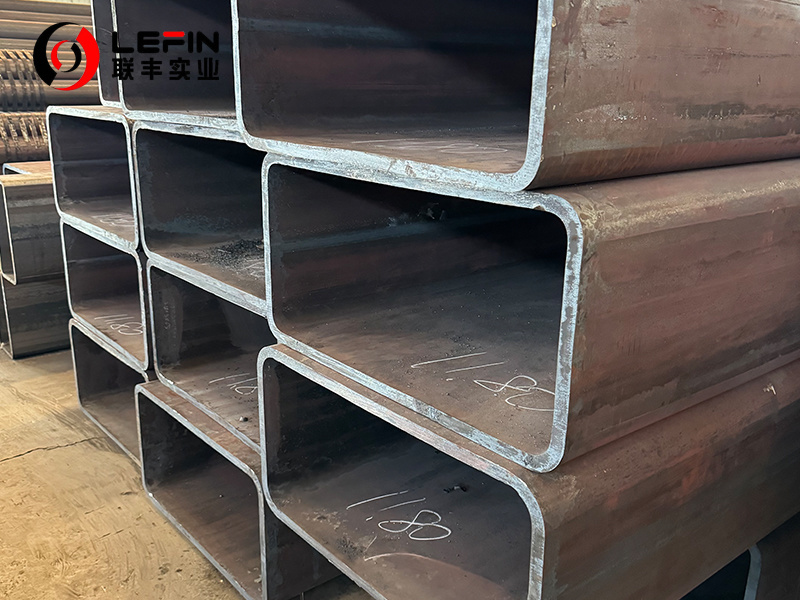
ASTM A501 GR.B TUBE
Size: Square Tube: 20MM * 20MM - 1200MM * 1200MM
Rectangular Tube: 20MM * 30MM - 1500MM * 1200MM
Wall Thickness: 1.3MM - 50MM
Length: 1M - 12M, normally 5.8M, 6M, 12M, also depends on the requirements.
Surface Treatment: Galvanizing, Black vanish, Carving, Slightly oil painting, PVC clothes cover each bundle etc.
Application: Bolted construction of bridges and buildings, as well as for General structural purposes.Chemical Composition
COMPOSITION, %
GRADE A
GRADE B,C
HEAT ANALYSIS
PRODUCT ANALYSIS
HEAT ANALYSIS
PRODUCT ANALYSIS
Carbon(C),max
0.26
0.30
0.22
0.26
Manganese(Mn),max
no requirement
no requirement
1.40
1.45
Phosphorus(P),max
0.035
0.045
0.030
0.040
Sulfur(S),max
0.035
0.045
0.020
0.030
Copper(Cu),min
0.20
0.18
0.20
0.18
Carbon (C): Lower carbon content compared to Grade C enhances weldability and reduces the risk of cracking during welding.
Manganese (Mn): Manganese improves strength and toughness, making the material more durable.
Phosphorus (P): Lower phosphorus content reduces the risk of brittleness and improves overall material quality.
Sulfur (S): Lower sulfur content enhances the material's ductility and reduces the risk of cracking.
Copper (Cu): Copper can improve corrosion resistance in certain environments.
Physical Requirements
ASTM A501 Tensile and Impact Requirements
Wall Thickness
GRADE A
GRADE B
GRADE C
TENSILE STRENGTH,min
All
58000psi
400MPa
65000psi
448MPa
70000psi
483MPa
WT≤25mm
39000psi
270MPa
46000psi
315MPa
50000psi
345MPa
25mm<WT≤50mm
38000psi
260MPa
45000psi
310MPa
49000psi
340MPa
YIELD STRENGTH,min
50mm<WT≤76mm
36500psi
250MPa
42500psi
290MPa
47500psi
330MPa
76mm<WT≤100mm
35000psi
240MPa
40000psi
280MPa
46000psi
315MPa
ELONGATION,min
25%
24%
23%
Tensile Strength: Minimum 65,000 psi (448 MPa). This high tensile strength ensures that the material can withstand significant loads without breaking.
Yield Strength: Minimum 46,000 psi (315 MPa) for wall thicknesses ≤ 1 inch (25 mm). The yield strength indicates the material's ability to deform elastically before plastic deformation occurs.
Elongation: Minimum 24%. This elongation value ensures that the material has good ductility, allowing it to be formed and bent without cracking.
Production Process
1.Raw Material Preparation: Steel is produced using basic-oxygen or electric-arc-furnace methods, ensuring it meets the chemical composition requirements for Grade B.
2.Tubing Formation: The steel is formed into tubes using methods such as seamless rolling, electric resistance welding (ERW), or submerged arc welding (SAW). The tubes are then hot-formed to achieve the desired shape and size.
3.Heat Treatment: For thicker-walled tubes (over 13 mm), normalizing heat treatment may be applied to ensure uniform mechanical properties.
4.Testing and Inspection: The tubes undergo chemical and mechanical testing to verify compliance with ASTM A501 Grade B standards. Surface quality checks and repairs are also performed.
5.Finishing: The final product may be coated for corrosion protection and marked with essential identification details.
ASTM A501 STEEL TUBE
Subcategory
Keyword
- Details
-
Brief Introduction
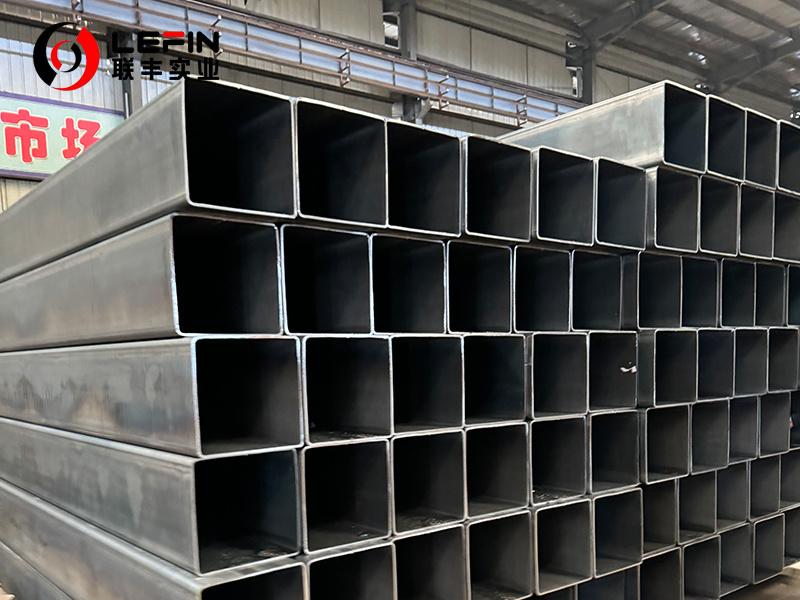
ASTM A501 GR.B TUBE
Size: Square Tube: 20MM * 20MM - 1200MM * 1200MM
Rectangular Tube: 20MM * 30MM - 1500MM * 1200MM
Wall Thickness: 1.3MM - 50MM
Length: 1M - 12M, normally 5.8M, 6M, 12M, also depends on the requirements.
Surface Treatment: Galvanizing, Black vanish, Carving, Slightly oil painting, PVC clothes cover each bundle etc.
Application: Bolted construction of bridges and buildings, as well as for General structural purposes.Chemical Composition
COMPOSITION, %
GRADE A
GRADE B,C
HEAT ANALYSIS
PRODUCT ANALYSIS
HEAT ANALYSIS
PRODUCT ANALYSIS
Carbon(C),max
0.26
0.30
0.22
0.26
Manganese(Mn),max
no requirement
no requirement
1.40
1.45
Phosphorus(P),max
0.035
0.045
0.030
0.040
Sulfur(S),max
0.035
0.045
0.020
0.030
Copper(Cu),min
0.20
0.18
0.20
0.18
Carbon (C): Lower carbon content compared to Grade C enhances weldability and reduces the risk of cracking during welding.
Manganese (Mn): Manganese improves strength and toughness, making the material more durable.
Phosphorus (P): Lower phosphorus content reduces the risk of brittleness and improves overall material quality.
Sulfur (S): Lower sulfur content enhances the material's ductility and reduces the risk of cracking.
Copper (Cu): Copper can improve corrosion resistance in certain environments.
Physical Requirements
ASTM A501 Tensile and Impact Requirements
Wall Thickness
GRADE A
GRADE B
GRADE C
TENSILE STRENGTH,min
All
58000psi
400MPa
65000psi
448MPa
70000psi
483MPa
WT≤25mm
39000psi
270MPa
46000psi
315MPa
50000psi
345MPa
25mm<WT≤50mm
38000psi
260MPa
45000psi
310MPa
49000psi
340MPa
YIELD STRENGTH,min
50mm<WT≤76mm
36500psi
250MPa
42500psi
290MPa
47500psi
330MPa
76mm<WT≤100mm
35000psi
240MPa
40000psi
280MPa
46000psi
315MPa
ELONGATION,min
25%
24%
23%
Tensile Strength: Minimum 65,000 psi (448 MPa). This high tensile strength ensures that the material can withstand significant loads without breaking.
Yield Strength: Minimum 46,000 psi (315 MPa) for wall thicknesses ≤ 1 inch (25 mm). The yield strength indicates the material's ability to deform elastically before plastic deformation occurs.
Elongation: Minimum 24%. This elongation value ensures that the material has good ductility, allowing it to be formed and bent without cracking.
Production Process
1.Raw Material Preparation: Steel is produced using basic-oxygen or electric-arc-furnace methods, ensuring it meets the chemical composition requirements for Grade B.
2.Tubing Formation: The steel is formed into tubes using methods such as seamless rolling, electric resistance welding (ERW), or submerged arc welding (SAW). The tubes are then hot-formed to achieve the desired shape and size.
3.Heat Treatment: For thicker-walled tubes (over 13 mm), normalizing heat treatment may be applied to ensure uniform mechanical properties.
4.Testing and Inspection: The tubes undergo chemical and mechanical testing to verify compliance with ASTM A501 Grade B standards. Surface quality checks and repairs are also performed.
5.Finishing: The final product may be coated for corrosion protection and marked with essential identification details.
Related products
Product Consulting
Address: Hengtai Road,Daqiuzhuang Town,Jinghai County,Tianjin,China
Mob: +8615122229899(whatspp)
Phone: +86 22 58171905
Fax: +86 22 58171902
E-mail:info@lefinsteel.com
Get company updates
Tianjin Lefin Industrial Co.,Ltd. All rights reserved City sub-station SEO www.300.cn