-
About us
 Tianjin lefin Industrial
TIANJIN LEFIN STEEL GROUP containing Tianjin lefin Industrial Co.,Ltd. 、Tianjin lefin steel import & export Co.,Ltd and Tianjin Shengqifeng International Trading Co., Ltd. -
Products
Steel Pipe Processing
Our main products include 1/2inch to 16 inch ERW PIPE/GI PIPE which has been produced according to BS1387/ASTM A53/EN10219/EN10255/EN10217 Standard -
-
Service Capability
Guarantee Quality
Our steel pipes are suitable for oil, natural gas, shipbuilding, chemical industry, water conservancy, electrical, steel structure, construction and other related fields.
What Causes Uneven Wall Thickness in Rolled Steel Pipes
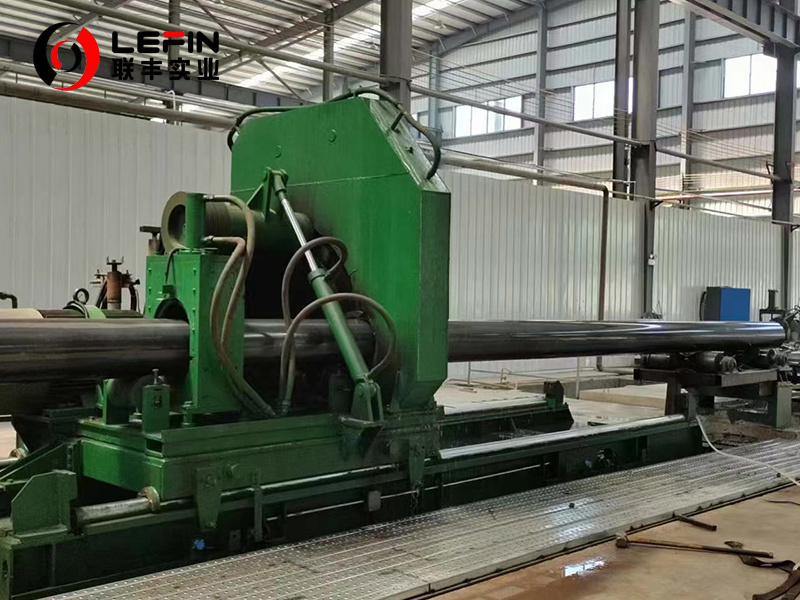
Uneven wall thickness in rolled steel pipes (especially seamless steel pipes, such as hot-rolled seamless steel pipes and cold-rolled seamless steel pipes) is a common quality issue in the production process. The core causes can be attributed to four major categories: raw materials, equipment, process, and operation. Specifically, it can be broken down into the following detailed factors, which are explained in detail in combination with the rolling principle (such as piercing, continuous rolling, and reducing core processes) :
I. Raw Material Factors: The "Inherent Basis" of Uneven Wall Thickness
Raw materials are the starting point of steel pipe rolling. If the raw materials themselves have defects, it will directly lead to deviations in the wall thickness of the finished product, and it is difficult to completely correct them in subsequent processes.
1. Quality problems of tube billets (steel billets)
- Uneven wall thickness/diameter of the tube billet :
The tube billet (such as round steel billet, continuous casting billet) itself has ellipticity, diameter fluctuations or local thickness/thinness (for example, the "loose zone", "shrinkage cavity", "segregation" of the continuous casting billet), and the metal deformation during rolling is inconsistent - the metal flow on the thicker side is blocked, and the flow on the thinner side is too fast, ultimately resulting in uneven wall thickness of the finished product.
- Internal defects of the tube billet :
The tube billet has inclusions, pores, cracks, etc. During the rolling process, the plasticity of the metal in the defect area is poor, and the deformation is not continuous, resulting in local wall thickness being too thin (the metal at the defect area cannot be effectively filled) or too thick (metal accumulates around the defect).
- Uneven tube billet temperature :
When the tube billet is heated (such as in a ring heating furnace), the heating is uneven, with local temperatures being too high (the metal is too soft, the flow is too fast) or too low (the metal is too hard, the flow is blocked), resulting in deviations in the wall thickness after rolling (for example, the upper part of the tube billet has a high temperature, but the wall thickness of the upper part is too thin after rolling).
2. Quality problem of the raw pipe (semi-finished product after perforation)
The first step in seamless steel pipe rolling is "piercing" (threading the tube blank into a hollow blank tube). If the wall thickness of the blank tube itself is uneven, it is difficult to completely correct it in the subsequent continuous rolling and sizing processes.
Improper adjustment of the cone Angle and the top position of the rolls in the piercing machine (such as the cross-rolling piercing machine) leads to "eccentric wall thickness" (one side thick and the other side thin) or "spiral uneven wall thickness" (alternating thickness in a spiral shape along the length of the steel pipe) in the rough pipe.
The ellipticity of the blank tube exceeds the standard: The cross-section of the blank tube is not round, and the metal deformation in the circumference direction during rolling is different, eventually resulting in uneven wall thickness.
II. Equipment factors: The "hardware guarantee" for rolling accuracy has failed
The precision, wear condition and alignment of the equipment directly determine the uniformity of metal deformation and are the core mechanical causes of uneven wall thickness.
1. Deviation/wear of core components of the rolling mill
- Roller problem :
The processing accuracy of the rolls themselves (such as the working rolls of continuous rolling mills and the rolls of sizing machines) is insufficient (such as inconsistent roll diameters and deviations in the cylindricity of the roll surface), resulting in uneven force on the metal during rolling.
Uneven wear of the rolls after use (such as severe wear on one side), inconsistent gap between the rolls (larger on one side and smaller on the other), and thickness deviation when metal passes through.
Uneven temperature of the rolls (such as blockage of the cooling waterway, local overheating and expansion) leads to changes in the actual roll gap.
- Top/mandrel issue :
The top of the piercing machine and the mandrel of the continuous rolling mill (used to support the inner wall of the steel pipe) are eccentric (not aligned with the centerline of the rolls), resulting in one side of the inner wall of the steel pipe being closely attached to the mandrel and the gap on the other side being too large, forming an "inner offset wall" (uneven thickness of the inner wall).
Wear, deformation of the mandrel (such as local thinning), or poor surface lubrication (metal adhesion) can cause local wall thickness deviation on the inner wall.
- Deviation of the guide guard device :
The guide and guard devices (such as guide plates and guide rollers) are used to guide the tube billet/blank tube into the rolls. If the position of the guide and guard is offset or the wear is uneven, it will cause the tube billet to "deviate", and during rolling, the metal force will be biased to one side, resulting in uneven wall thickness.
2. Failure of equipment alignment/levelness
The levelness and verticality deviations of the rolling mill frame and base (such as foundation settlement and bolt loosening after long-term use) result in the centerlines of the rolls and mandrels not being aligned (poor alignment), and the metal deformation is asymmetrical.
The centerlines of each stand of the multi-stand continuous rolling mill are not aligned (longitudinal alignment is poor), and the blank tubes are repeatedly "squeezed and deflected" when passing through, resulting in periodic uneven wall thickness along the length direction.
3. Synchronization problem of the transmission system
Faults in the transmission components of the rolling mill such as the motor, reducer and coupling (such as inconsistent rotational speed and excessive transmission clearance) cause the rotational speeds of each roll to be out of sync, resulting in the metal being "pulled" or "unevenly squeezed", and causing fluctuations in wall thickness.
III. Process factors: Improper "parameter matching" during the rolling process
Process parameters are the key to controlling metal deformation. Unreasonable parameter Settings can lead to mismatches in deformation amount, temperature and speed, causing uneven wall thickness.
1. Improper temperature process
- Heating temperature deviation :
If the heating temperature of the tube blank is too high (overheating), the metal will have excessive plasticity, which can easily lead to "overdeformation" (local thinning). When the temperature is too low (underheated), the plasticity of the metal is poor, the deformation resistance is large, and "hard squeezing" (local thickness) is prone to occur.
Insufficient heating time or uneven heat preservation, excessive temperature difference between the inside and outside of the tube billet or between the top and bottom (such as too dense stacking of tube billets in a ring heating furnace), and uneven deformation during rolling.
- Failure of temperature control during rolling process :
When the rough pipe is rolled and cooled too quickly (such as with excessive cooling water or uneven cooling), the local metal hardens prematurely, making subsequent deformation difficult and resulting in wall thickness deviation.
During continuous rolling, the temperature fluctuations between each frame are too large (for example, the outlet temperature of the front frame is too high, and the deformation of the rear frame during rolling is excessive).
2. Deformation parameters do not match
- Improper setting of the roll gap:
The roll gap is a core parameter that determines the wall thickness of the steel pipe. If the gap on one side is too large during the adjustment of the roll gap (such as not calibrating according to the actual size of the blank pipe), or the roll gap Settings of each frame are not continuous (such as a large roll gap in the front frame and a small roll gap in the rear frame), it will cause a sudden change in the metal deformation and uneven wall thickness.
- Unreasonable elongation coefficient:
The elongation coefficient (the ratio of the length after rolling to the length before rolling) is too large or too small, or the elongation coefficient is unevenly distributed among each frame - if the elongation coefficient is too large, the metal flows too fast, which is prone to local thinning. Uneven distribution will lead to differences in the deformation amount of each section, resulting in fluctuations in wall thickness.
- Improper speed parameters:
The feeding speed of the billet (piercing speed), the rotational speed of the rolls, and the extraction speed of the mandrel do not match, resulting in insufficient metal supply or accumulation. For instance, if the piercing speed is too fast and the mandrel support is not timely, the inner wall of the steel pipe will become locally thinner.
3. Failure of lubrication/cooling process
Insufficient lubrication during rolling (such as insufficient lubricating oil or deteriorated grease) leads to excessive friction between the metal and the rolls or mandrel, resulting in increased resistance to local deformation and a thicker wall thickness.
Uneven cooling process (such as blockage of cooling waterways, deviation of nozzle angles), rapid local cooling of the steel pipe surface, increased hardness, and inability to effectively correct it in subsequent processes, resulting in wall thickness deviation.
IV. Operational factors: The "precision execution" controlled by humans is not in place
The skills of the operators, the timeliness of inspection and adjustment directly affect the execution effect of the process and are the "human causes" of uneven wall thickness.
1. Error in parameter adjustment
The operator failed to adjust parameters such as the roll gap, rotational speed, and temperature according to the specifications and materials of the tube billet (for instance, using the old parameters to produce steel pipes of different specifications), resulting in a mismatch between the parameters and the raw materials.
When adjusting the roller gap, it was not calibrated (such as only adjusting based on experience without using tools like a dial indicator for measurement), resulting in a deviation between the actual roller gap and the set value.
2. Inspection and maintenance are not timely
- The wear conditions of components such as rolls, mandrels, and guide guards were not inspected regularly (for instance, the rolls were not replaced when the wear exceeded the standard), or the metal adhesions and oxide scales on the surface of the components were not cleaned in time, resulting in uneven deformation.
- Failure to detect equipment alignment deviations in a timely manner (such as frame offset, loose guide guards), or failure to make timely adjustments after discovery.
3. The selection of raw materials is not strict
The operators failed to conduct appearance and dimensional inspections on the tube billets (such as using tube billets with excessive ellipticity), resulting in "inherent defects" flowing into the rolling process.
V. Typical Causes of Uneven Wall Thickness Due to Different Rolling Processes (Summary Table)
| Rolling process: | Typical forms of uneven wall thickness; | Core causes |
| Hot-rolled seamless steel tubes (piercing + continuous rolling) | Eccentric wall (thickness/thinness on one side) | Uneven heating of the billet, eccentricity of the piercing machine top head, poor alignment of the continuous rolling mill, uneven wear of the rolls |
| Uneven wall thickness in the spiral shape | Improper cone Angle of the punching machine roller, offset of the guide guard device, and deviation of the rough pipe | |
| Periodic fluctuations in wall thickness | The rotational speeds of each frame of the continuous rolling mill are not synchronized, the roll gap Settings are not continuous, and the mandrels are unevenly worn | |
| Cold-rolled seamless steel pipe | Inner offset wall (uneven thickness of the inner wall) | mandbar eccentricity, poor alignment of the cold rolling mill rolls, insufficient lubrication leading to metal adhesion |
| Local thin dots/thick dots | Local defects in raw materials (blank tubes), impurities adhering to the surface of the rolls, and uneven cooling | |
| Sizing/reducing process | The wall thickness at the end is uneven | The temperature at the end of the blank pipe is too low, the roller gap of the sizing machine is improperly adjusted, and the guiding deviation of the guide guard |
impurities adhering to the surface of the rolls, uneven cooling
Sizing/reducing process: Uneven wall thickness at the end, too low temperature at the end of the blank pipe, improper adjustment of the roller gap of the sizing machine, deviation of the guide and guard

VI. How to Identify and Solve Uneven Wall Thickness? (Brief guidance)
1. Detection and positioning :
Use an ultrasonic thickness gauge to measure along the circumference of the steel pipe (at least four directions) and the length direction (every 100-200mm) to determine the form of non-uniformity (eccentricity, helical, periodic).
2. Targeted Investigation:
- Eccentric wall: Prioritize checking the equipment's alignment (roller-mandbar centerline), eccentricity of the top/mandbar, and uneven heating of the tube billet.
- Uneven spiral shape: Check the guide guard of the punching machine, the cone Angle of the rolls, and the deviation of the blank pipe.
- Periodic fluctuations: Check the synchronization of the continuous rolling mill speed, the wear cycle of the rolls, and the setting of the roll gap.
3. Solutions:
- Raw materials:
Screen qualified tube billets (with uniform size and temperature), and remove defective raw materials;
- Equipment:
Calibrate alignment and levelness, replace worn parts (rolls, mandrels, guide guards), and clean the surfaces of components;
- Process:
Optimize heating temperature (uniform insulation), adjust the roller gap/speed matching, and improve lubrication and cooling;
- Operation:
Strengthen inspection (calibrate parameters and check equipment status for each batch), and enhance the skills of operators.
From the above analysis, it can be seen that the uneven wall thickness of rolled steel pipes is the result of the coordinated failure of multiple links such as "raw materials - equipment - process - operation", and the core lies in the destruction of the uniformity of metal deformation. In production, full-process control from "source (raw materials) - process (equipment + technology) - execution (operation)" is necessary to effectively reduce the probability of uneven wall thickness.
Address: Hengtai Road,Daqiuzhuang Town,Jinghai County,Tianjin,China
Mob: +8615122229899(whatspp)
Phone: +86 22 58171905
Fax: +86 22 58171902
E-mail:info@lefinsteel.com
Get company updates
Tianjin Lefin Industrial Co.,Ltd. All rights reserved City sub-station SEO www.300.cn